Views: 0 Author: Site Editor Publish Time: 2026-10-16 Origin: Site
For large-scale architectural projects or wholesale distributions, subtle color shifts in an exterior cladding order can lead to rejected installations. Delayed handovers and severe financial liabilities often follow. You might think panels look identical in the factory, only to discover obvious discrepancies once they hang on a sunlit facade.
Visual matching is subjective and insufficient for multi-batch production. Variations in curing temperatures, paint chemistry, and coil coating speeds naturally cause deviations. Relying on the naked eye creates unacceptable project risks. Different production runs inherently possess slight differences, and ignoring this reality compromises the entire architectural vision.
We aim to provide procurement teams, architects, and fabricators with an objective, data-driven framework. You will learn how to evaluate a manufacturer’s quality control (QC) infrastructure and testing capabilities before finalizing a contract. This guide equips you to mandate strict tolerances, ensuring perfect visual harmony across massive building facades.
Understanding why colors shift between production runs helps you manage expectations. It also allows you to pinpoint where a manufacturer might fail during quality control. The manufacturing process involves dynamic chemical and mechanical variables. Even minor fluctuations produce visible differences on a finished colored aluminum composite panel.
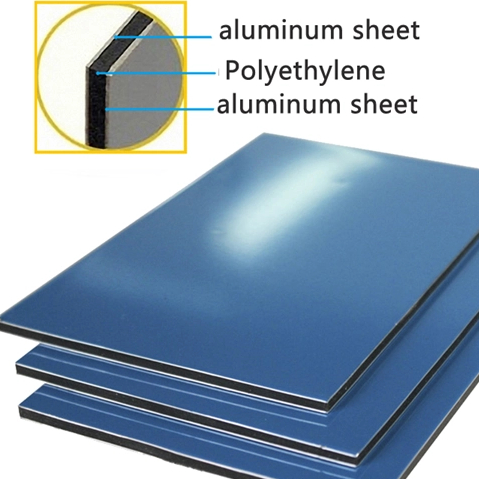
Paint systems rely on complex chemical formulations. Variations in raw pigment batches directly impact the final shade. Different resin ratios, especially when comparing PVDF to PE, alter how the paint absorbs and reflects light. Furthermore, solvent evaporation rates change based on factory humidity and ambient temperature. When solvents evaporate too quickly or too slowly, they leave distinct textural micro-patterns on the surface. These patterns subtly change how we perceive the hue.
Coil coating is a continuous, high-speed industrial process. Fluctuations in oven curing temperatures affect how the paint bakes onto the aluminum skin. If the temperature drops by just a few degrees, the resin might not cure uniformly. Line speed and roller pressure also determine the final film build. A thicker film can look darker, while a thinner film might expose the primer beneath. These mechanical variables directly alter the final gloss level and pigment density.
Solid paints are relatively straightforward to match. Metallic finishes introduce a significant challenge known as the "flop effect." Metallic paints contain tiny aluminum flakes. During the roller coating process, these flakes lay down in a specific direction. They act like microscopic mirrors reflecting light. If you view the panel from a different angle, or if a subsequent batch aligns the flakes differently, the panels will look mismatched. This optical shift happens even if the chemical paint formula remains perfectly identical.
Failing to control these variables leads to costly post-installation remediation. Imagine discovering a checkerboard effect on a fifty-story high-rise. Removing and replacing panels requires scaffolding, labor, and new materials. The legal risks of failing to meet architectural specifications are equally severe. Clients routinely withhold payments until facades meet exact visual standards. Consequently, proactive quality control saves millions of dollars.
Human eyesight is an unreliable metric for quality control. Fatigue, lighting conditions, and individual biology change how we see colors. To eliminate subjectivity, the architectural industry relies on the CIELAB color space and Delta E (ΔE) measurements.
The CIELAB color space maps every color across three numerical axes. 'L' measures lightness to darkness. 'a' measures green to red. 'b' measures blue to yellow. Delta E (ΔE) calculates the mathematical distance between two colors within this space. For architectural cladding, a ΔE of ≤ 1.0 to 1.5 is the standard threshold. A ΔE below 1.0 is generally imperceptible to the human eye. Pushing the standard beyond 1.5 usually results in noticeable facade variations.
Table: Delta E (ΔE) Acceptability Chart for Architectural Panels
| Delta E (ΔE) Value | Visual Perception | Architectural Suitability |
|---|---|---|
| 0.0 - 0.5 | Indistinguishable to the naked eye. | Ideal for premium, high-visibility commercial facades. |
| 0.6 - 1.0 | Barely perceptible under close inspection. | Standard requirement for strict architectural specifications. |
| 1.1 - 1.5 | Slight difference visible to trained professionals. | Acceptable for most wholesale and standard projects. |
| 1.6 - 2.5 | Noticeable difference under normal lighting. | High risk of rejection for continuous flat facade designs. |
| > 2.5 | Distinct, obvious color mismatch. | Unacceptable. Panels should be rejected by QC. |
The limitations of human eyesight become obvious when dealing with metamerism. Metamerism occurs when two objects appear to match under one light source but clash under another. For instance, panels might look identical under factory fluorescent lights. However, they may look completely different under natural sunlight. Objective digital measurement eliminates this risk. It scores the color mathematically, ignoring ambient factory lighting tricks.
Top-tier suppliers utilize calibrated spectrophotometers at multiple production stages. They do not just check the final product. Effective ACP color matching requires testing the initial lab dip, monitoring the continuous production line, and conducting final QA before packaging. Using brands like Datacolor or X-Rite ensures the hardware meets global calibration standards. If a supplier does not own this equipment, they are guessing.
While instruments handle the primary data, secondary visual checks remain part of standard QA protocols. However, you must perform these checks under standardized lighting. Suppliers should use D65 daylight viewing booths. These controlled environments replicate natural midday sunlight. They allow inspectors to catch obvious gloss discrepancies or metallic flop issues that instruments occasionally miss.
A flawless facade design rarely consists only of flat panels. Buildings require window flashings, custom extrusions, and complex edge trims. Integrating these different components is where many projects fail visually. Coordinating these elements requires early planning and strict material synchronization.
Matching continuous coil-coated sheets with spray-coated aluminum extrusions presents inherent difficulties. Coil coating applies paint under immense roller pressure. It creates a tightly bonded, highly uniform film. Conversely, spray coating is either manual or electrostatic. It results in a thicker, slightly more porous film build. These distinct application methods cause the paint to cure differently. The same liquid paint often looks noticeably different once dried on these two separate substrates.
To mitigate material differences, mandate a unified paint system. The same paint formulation and manufacturer (e.g., PPG, Beckers) must be used across all facade components. Never let your extrusion fabricator buy a "similar" color from a local vendor. You must specify the exact pigment codes and resin bases used by the panel manufacturer.
Consider these best practices for trim integration:
Differing gloss percentages between panels and accessories ruin matching efforts. If your panel has a 30% gloss level, but the flashing has a 50% gloss level, they will look mismatched. The base pigment could be identical, but the way they reflect light creates an optical illusion of a color clash. Always specify and verify the gloss tolerance alongside the Delta E tolerance.
Procuring a massive order based on a tiny printed brochure is a recipe for disaster. Trustworthy suppliers invite scrutiny. They offer transparent, highly documented processes. You must systematically evaluate how they manage quality from the initial request to the final shipping pallet.
Never rely on digital renders or standard RAL/Pantone paper chips. Digital screens emit light, while building facades reflect it. Paper chips have different textures than metal. Buyers must mandate and sign off on physical, lab-generated draw-down panels. These samples use the actual aluminum substrate and the proposed paint chemistry. This physical prototype is your only reliable baseline.
Ask potential suppliers how they catch errors during a production run. Quality control processes must feature automated, real-time color monitoring.
This automated loop catches deviations instantly, preventing thousands of defective square meters from being packaged.
A rigorous QA system leaves a paper trail. Suppliers must provide complete audit trails for your order. This documentation should include date stamps, paint batch numbers, and specific ΔE readouts for every pallet shipped. If a panel arrives damaged on-site six months later, this traceability allows the manufacturer to reproduce the exact shade using the historical batch data.
You have learned the science behind color consistency. Now, you must translate that knowledge into contractual obligations. The procurement phase is your opportunity to lock in strict tolerances and minimize liability. A reputable supplier of a colored aluminum composite panel will welcome these detailed requirements.
Vague language protects the manufacturer, not you. Do not accept terms like "commercially reasonable match" or "visually similar." Instead, embed specific numerical limitations into the procurement contract. State clearly that "all panels must maintain a ΔE of ≤ 1.5 against the approved master sample." Furthermore, specify the testing methods and hardware brands (e.g., CIELAB D65 illumination) used to settle disputes.
Check the fine print regarding the warranty lifespan. Focus heavily on color retention and chalking clauses. Paint naturally degrades under UV exposure. However, standard PVDF coatings should fade uniformly. Ensure the warranty clearly outlines liability for severe batch mismatches that become apparent only after a year of weathering. Understand who bears the cost of scaffolding and labor if panels need replacing.
Accidents happen on construction sites. Forklifts damage panels, or installers cut them incorrectly. Evaluate the supplier’s policy and lead times for matching a new panel to an already-installed facade. You must account for UV degradation. A freshly painted panel will not match a panel that has baked in the sun for two years. Ask how the supplier handles this on-site spectrophotometry and custom matching process.
Before placing a bulk order, test the supplier's responsiveness. Request a custom color match sample. See how long they take to produce the physical lab dip. Review their ISO 9001 quality management certifications. An ISO-certified facility proves they have standardized operating procedures for handling raw materials, maintaining ovens, and calibrating testing equipment.
Do not skip these validation steps. The extra weeks spent testing a supplier’s capabilities save months of legal disputes and project delays during installation.
Consistent cladding aesthetics are not an art; they represent a strictly controlled industrial science. Manufacturers manage variables from chemical resin structures to oven baking temperatures. Relying on verbal assurances without contractual ΔE tolerances exposes projects to unnecessary risk. You must demand objective, instrument-verified data.
Prioritize suppliers who offer transparent QA data and comprehensive physical prototyping. Demand physical draw-down samples on actual aluminum substrates. Verify their in-line monitoring capabilities. Treat the integration of flashing and trims with the same rigor as the main panels.
Contact our technical team to request a custom lab dip sample or consult on establishing strict color tolerances for your next high-volume facade project. We provide the expertise needed to secure flawless architectural finishes.
A: For standard architectural applications, a ΔE of ≤ 1.5 is the acceptable threshold. At this level, variations are generally imperceptible under normal lighting. However, for highly critical, premium commercial facades with continuous flat surfaces, projects may demand a stricter tolerance of ≤ 1.0 to ensure absolute visual uniformity.
A: Metallic finishes contain tiny aluminum flakes that act as directional mirrors. During roller coating, these flakes align uniformly. This creates the flop effect, where light reflects differently based on the viewing angle. You must install panels strictly according to the directional arrows printed on the protective film to avoid perceived shade variation.
A: Yes, but it is complex. Matching new paint to UV-faded panels requires physical on-site sample spectrophotometry. You cannot use the original factory color code, as the building's color has drifted due to sun exposure. The manufacturer needs an actual weathered panel offcut to perform a custom lab match.
A: Realistic commercial timelines for custom lab dips typically range from 7 to 14 days. This timeline depends on formulation complexity, pigment availability, and the specific resin system required (e.g., PVDF vs. PE). Multiple iterations may be needed to hit a strict ΔE tolerance.